Cost and Lead Time for Castings with Custom Finishing
Post-casting finishing significantly affects total cost and delivery. Foundry selection requires evaluating supplier evaluation criteria for finishing capabilities, process stability, and transparent pricing to ensure your project meets budget and schedule targets.
- Finishing operations add cost and time that must be included in the total project budget.
- Clear RFQs specifying finishing requirements improve the accuracy of supplier evaluation.
- Comparing quotes fairly requires aligning scope, material, and finishing specifications.
- Foundry selection should prioritize communication, process stability, and realistic lead time commitments.
How Finishing Changes the Total Cost
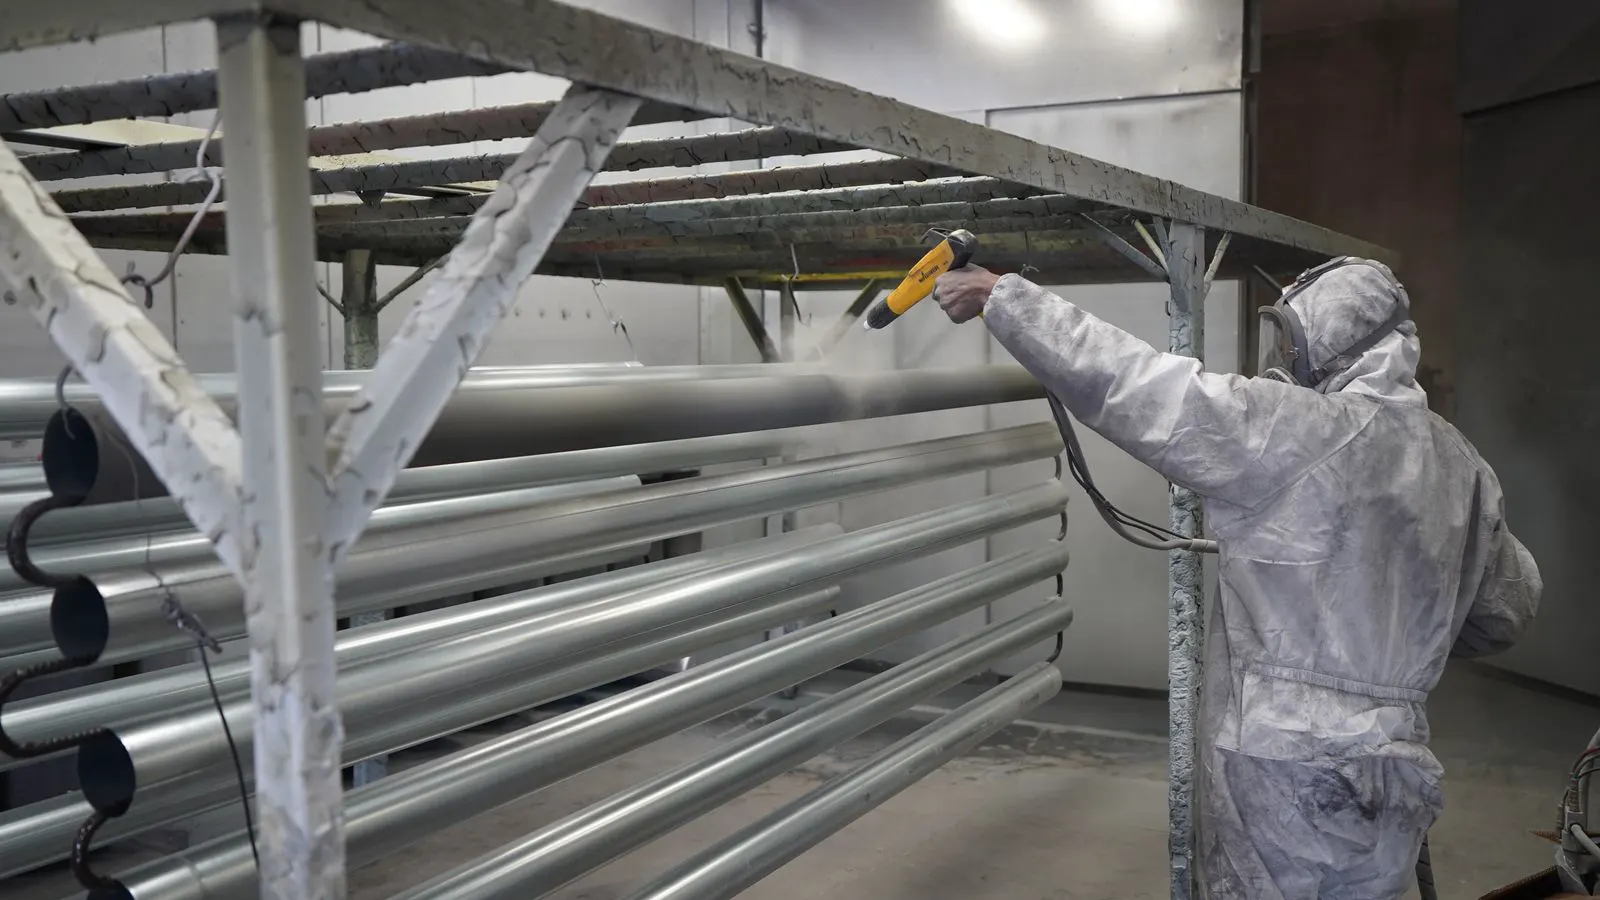
Finishing is where project budgets often drift. A foundry quote covers the melt, mold, and core work, but the final part may require machining, heat treatment, deburring, or surface coating. Each step adds labor, material, and inspection time. If the RFQ does not list these operations, the foundry will add them later.
A typical investment casting project involves a machined bracket, a valve body, or a structural component. The base casting cost covers the raw material and the investment process. Finishing costs then stack on top. A part that needs only deburring and cleaning has a lower finishing cost than a part that requires CNC machining, anodizing, and a final dimensional check.
The key is to define the finishing scope before sending the RFQ. Vague instructions like “finish to drawing” lead to different interpretations. One foundry may assume the drawing includes all machining tolerances. Another may assume the customer will handle surface treatment. The result is a price gap that has nothing to do with the foundry selection process.
What Drives Finishing Prices
Finishing prices are driven by several factors. The first is the operation type. Deburring and cleaning use hand tools and simple abrasives. Machining requires CNC setups, tooling, and operator time. Heat treatment needs controlled ovens and specialized personnel. Each operation has a different cost structure.
The second factor is tolerance. Tighter tolerances require more setup, slower feed rates, and more inspection. A part machined to a loose tolerance can be produced quickly. A part machined to a tight tolerance may require multiple operations and final verification. The foundry selection process must account for these differences.
The third factor is material. Some alloys are harder to machine. Some require specific heat treatment cycles. The material choice affects tool wear, cycle time, and post-process inspection. When comparing quotes, ensure the material grade is identical across all proposals.
The fourth factor is volume. Small batches have higher per-unit finishing costs. Large batches spread setup and labor costs over more units. A foundry selection strategy should consider volume flexibility. A supplier that can handle both small prototype runs and production volumes offers more predictable cost behavior.
How to Write a Clear RFQ for Finishing
A clear RFQ removes ambiguity. Start with the part geometry and material. List all finishing operations with specific requirements. Use a table in the RFQ to separate the casting requirements from the finishing requirements.
For example, specify “Deburr all edges to 0.5 mm radius” rather than “deburr.” Specify “Machining to drawing with 0.1 mm tolerance” rather than “machine to drawing.” Specify “Heat treat to 302-304 hardness” rather than “harden.”
Include the drawing number and revision. Attach the drawing or provide a link. State the required inspection level. If the customer requires a first article inspection, say so. If the customer requires a material test report, say so.
The RFQ should also state the required delivery date. This forces the foundry to plan the finishing sequence. If the foundry cannot meet the date, they should state it clearly. This is a key part of supplier evaluation. A foundry that commits to a date it cannot meet creates schedule risk.
How to Compare Quotes Fairly
Comparing quotes requires alignment. Do not compare a quote that includes machining with a quote that does not. Do not compare a quote for aluminum with a quote for stainless steel. Do not compare a quote for one year with a quote for three years.
Create a comparison matrix. List each foundry in a row. List each cost component in a column. Columns should include material, casting labor, finishing labor, tooling, inspection, and overhead. This forces a transparent view of where each foundry differs.
Review the lead time breakdown. Ask each foundry to split the lead time into phases: design review, mold making, casting, finishing, and inspection. This shows where the schedule risk lies. A foundry with a fast casting process but a slow finishing process may not deliver on time.
Check the payment terms. Some foundries require full payment upfront. Others offer net terms. Payment terms affect cash flow. Include this in the supplier evaluation. A lower quote with harsh payment terms may not be the best choice.
Lead Time and the Finishing Sequence
Finishing often determines the total lead time. The casting process may take two weeks. Finishing may take three weeks. Inspection may take one week. The total is six weeks. If the finishing operations are sequential, the lead time adds up. If they are parallel, the lead time shrinks.
A foundry selection process should ask about parallel processing. Can deburring and cleaning happen while another part is being machined? Can heat treatment start while machining is being set up? The answer affects delivery speed.
Communication is critical. The foundry must report finishing progress. A weekly status update on finishing operations helps the customer track the project. If a finishing step runs late, the customer needs to know early. This is why the foundry selection process must include communication checks.
Cost and Lead Time Trade-Offs
There is always a trade-off between cost and speed. Rushing a finishing operation costs more. It may require overtime, expedited tooling, or parallel processing. The customer pays a premium for speed. The foundry must balance this premium with its capacity.
If the project has a fixed delivery date, the cost of rush processing must be accepted. If the project has a flexible date, the customer can save money by allowing standard lead times. The foundry selection process should reflect this reality. A supplier with a long standard lead time may be the best choice for a non-urgent project. A supplier with a short rush lead time may be the best choice for a critical project.
The customer should state the urgency in the RFQ. If the part is for a prototype, the lead time may be flexible. If the part is for a production line, the lead time is fixed. The foundry selection process should match the supplier’s capability to the project’s urgency.
Supplier Evaluation for Finishing Capability
Supplier evaluation must go beyond the casting floor. The foundry must have the finishing capability in-house or through a qualified partner. In-house finishing gives more control. Partner finishing may add cost and communication lag.
Ask the foundry to list its finishing operations. Ask for a sample of a finished part. Ask for the inspection method. Ask for the material test procedure. These questions reveal the depth of the foundry’s finishing capability.
A foundry that can explain its finishing process in detail is a better candidate than a foundry that gives vague answers. The foundry selection process should include a site visit or a video call to discuss finishing. This interaction helps build trust and clarifies expectations.
Cost and Lead Time Summary Table
The table below summarizes the main cost drivers and lead time factors for finishing. Use this table when reviewing quotes and planning the project.
| Cost Driver | Description | Lead Time Impact |
|---|---|---|
| Operation Type | Deburring, machining, heat treatment, coating | Sequential operations add time |
| Tolerance | Tighter tolerances require more setup and inspection | Slower cycle times |
| Material | Harder materials require specialized tools and processes | Increased tooling and setup |
| Volume | Small batches have higher per-unit costs | Setup time dominates |
| Inspection | First article and final inspection | Adds verification time |
Final Checks Before Selection
Before finalizing the foundry selection, run a final check. Review the RFQ for completeness. Confirm the finishing scope. Confirm the material grade. Confirm the inspection requirements. Confirm the delivery date.
Review the quote for transparency. Ensure all cost components are listed. Ensure the lead time breakdown is clear. Ensure the payment terms are acceptable.
Review the communication plan. Agree on the reporting frequency. Agree on the escalation path. Agree on the documentation requirements.
The foundry selection process is about risk reduction. By defining the finishing scope, comparing quotes fairly, and evaluating supplier capability, the customer reduces the risk of budget overruns and delivery delays. The result is a project that stays on budget and on schedule.
Frequently asked questions
How do I estimate finishing costs in a foundry selection process?
Define each finishing operation in the RFQ. Ask for a line-item quote for each operation. This allows for a fair comparison across suppliers.
Can finishing be done in-house or by a partner?
Both options exist. In-house finishing offers more control. Partner finishing may add cost and communication lag.
What is the biggest cause of finishing cost overruns?
Ambiguous requirements. Vague instructions lead to different interpretations and added work.
How does tolerance affect lead time?
Tighter tolerances require more setup, slower feed rates, and more inspection. This increases the cycle time.
What should I check in supplier evaluation for finishing?
Check the finishing capability, inspection method, and communication plan. Ask for a sample of a finished part.