Checklist: Verifying Foundry Burnout and Preheating
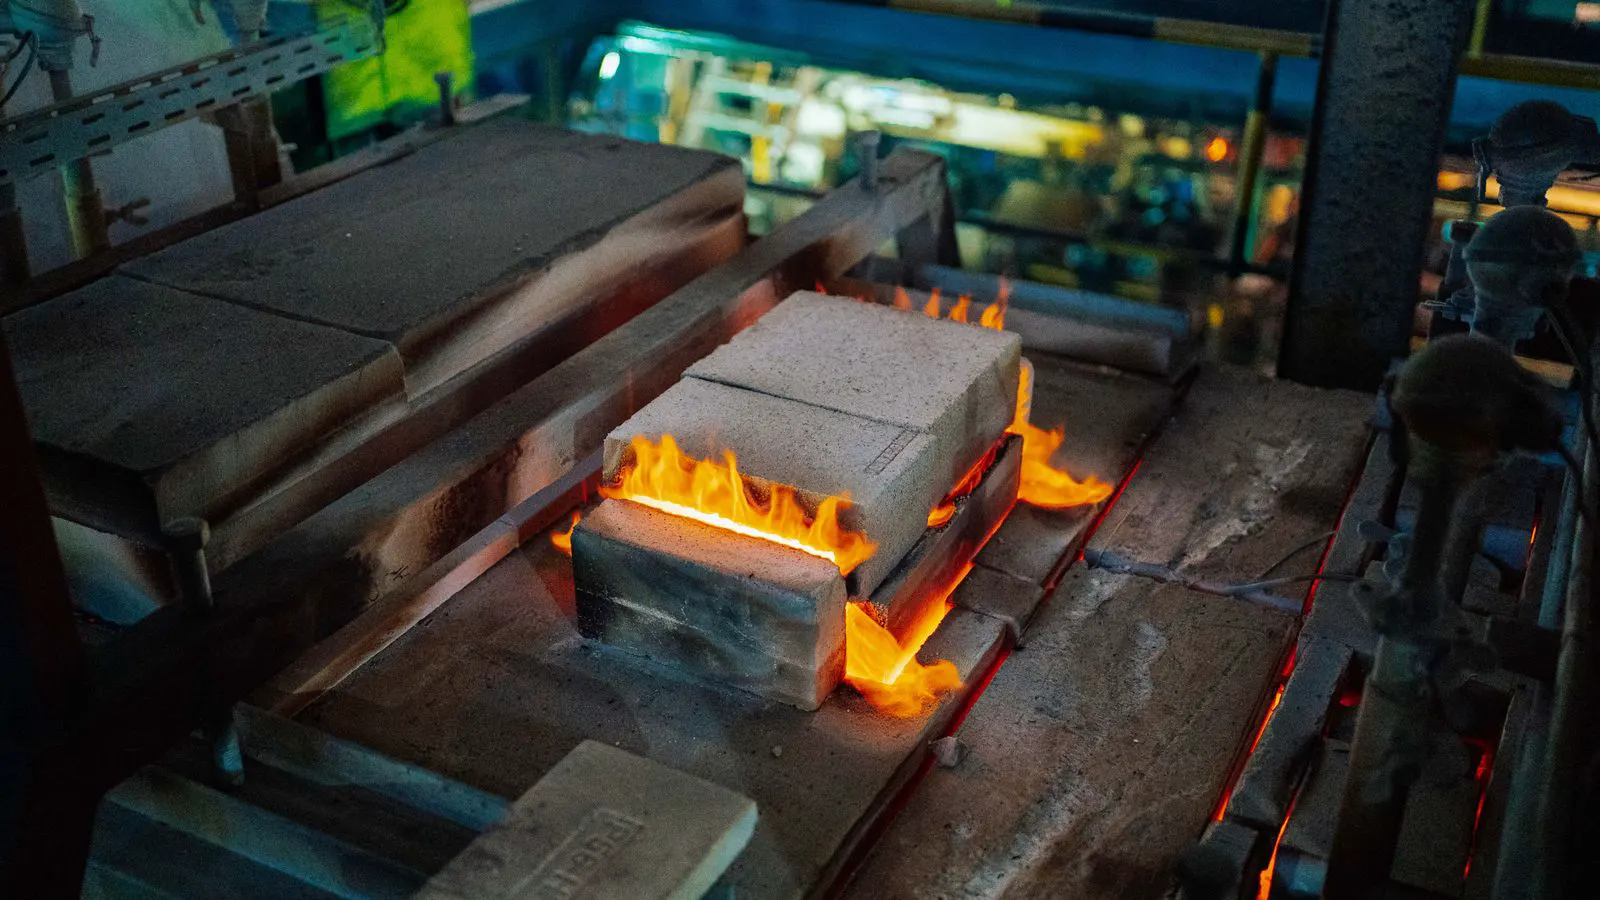
Use a structured audit to confirm wax recovery, preheating process, and mold integrity before production. This checklist helps buyers and engineers identify red flags that cause gas porosity and other casting defects.
- Verify burnout temperature and time against the foundry standard work instruction.
- Check mold integrity after preheating to confirm no structural damage.
- Review wax recovery records to ensure complete removal before investment.
- Confirm preheat temperature and ramp rates match the alloy requirements.
- Track red flags like venting issues, mold cracking, or inconsistent heat soak.
Why Burnout Verification Matters
Gas porosity often starts long before the pour. A residual wax pocket in the mold releases trapped gas when it hits metal temperature. That gas can expand into the casting and create a void. The result is a part that fails inspection.
Buyers and engineers need a repeatable way to confirm the foundry actually performed the burnout and preheating process correctly. The audit below focuses on the physical and documentary evidence of those steps. It is not a substitute for the foundry internal controls. It is a buyer side check to ensure the process was executed as promised.
Confirming Wax Recovery and Burnout Execution
The first step is to verify the wax pattern was completely removed from the mold before investment was applied. This is where wax recovery matters most. If the foundry uses a chemical or thermal process, the documentation should show the specific method used.
Check the following:
- Burnout temperature and time logs: The foundry should record the maximum temperature reached and the duration of the heat soak. The values must match the standard work instruction for the specific alloy and wax type.
- Mold venting records: Confirm the vents were open and clear during burnout. Blocked vents trap steam and gas. Those gases can become trapped in the mold and migrate into the casting.
- Wax recovery method: If the foundry recovers wax, check the records for the recovery rate. A consistent recovery rate indicates the process is stable. A sudden drop may signal incomplete removal or a change in wax composition.
- Mold inspection after burnout: The foundry should visually or mechanically inspect the mold after burnout. Look for cracks, slumping, or residue. Residue indicates the wax was not fully removed.
Red Flags in Burnout Documentation
Do not assume the logs are clean just because they exist. Look for gaps and inconsistencies.
- Missing temperature data: If the log shows only start and end times, but no temperature readings, the audit cannot verify the burnout.
- Inconsistent heat soak times: If one mold set burns for 8 hours and another for 3 hours without a documented reason, there is a process variation.
- No venting confirmation: If there is no record that vents were checked before and after burnout, the risk of gas entrapment rises.
- Chemical burnout without residue testing: If the foundry uses a chemical wash, but there is no test for residual wax, the risk of gas porosity remains high.
Preheating Process and Temperature Control
The preheating process is often misunderstood. It is not just about warming the mold. It is about controlling the thermal shock when the metal enters the mold. The preheat temperature and ramp rate must match the alloy. Too low a preheat causes the mold to crack or the metal to solidify too fast. Too high a preheat can distort the mold or degrade the investment.
The checklist below verifies the preheating process was executed correctly.
- Preheat temperature records: The foundry should log the actual temperature of the mold before the pour. Compare it to the target temperature for the alloy.
- Ramp rate documentation: Check if the foundry records how quickly the mold was heated. A fast ramp can cause thermal shock. A slow ramp is safer but increases cycle time.
- Mold stability check: After preheating, the foundry should confirm the mold did not shift or crack. A cracked mold will leak during the pour.
- Investment compatibility: Verify the investment material was rated for the preheat temperature. If the investment was not tested at that temperature, the risk of delamination or cracking increases.
Mold Integrity After Preheating
The preheating process can weaken the mold. Investment casting molds are fragile. They must hold their shape under heat and pressure. A buyer audit should confirm the foundry checked the mold after preheating.
Look for these physical checks:
- Crack inspection: The foundry should visually inspect the mold for hairline cracks. Cracks can form during preheating if the ramp rate was too fast.
- Dimensional stability: Check if the mold dimensions are still within tolerance. Thermal expansion and contraction can shift the mold. If the dimensions are out of spec, the part will be out of spec.
- Surface condition: Look for slumping or erosion on the mold surface. Erosion indicates the investment was not strong enough for the preheat temperature.
Comparing Burnout and Preheating Records
A single set of logs is not enough. The buyer should cross-reference the burnout records with the preheating records. The two processes must be linked to the same mold set.
Use this table to compare the data:
| Check Item | Burnout Record | Preheating Record | Red Flag |
|---|---|---|---|
| Mold Set ID | Listed | Listed | Missing ID |
| Max Temperature | Recorded | Recorded | Temperature gap |
| Time Duration | Recorded | Recorded | Missing time |
| Vent Status | Open | Open | Vent blocked |
| Mold Inspection | Passed | Passed | Crack noted |
If the burnout record shows a mold set that does not appear in the preheating record, the foundry may have skipped a step. If the preheat temperature is significantly higher than the burnout temperature without a documented reason, the mold may be damaged.
Final Audit Checklist for Buyers
Use this numbered list to complete the audit on site or with digital records.
- Verify the wax recovery method and recovery rate.
- Confirm burnout temperature and time logs match the standard work instruction.
- Check venting records for all mold sets.
- Review preheating temperature and ramp rate data.
- Inspect mold integrity after preheating.
- Cross-reference burnout and preheating records by mold set ID.
- Confirm the investment material is rated for the preheat temperature.
When to Escalate
If the audit finds multiple red flags, escalate the issue. A single missing data point may be a clerical error. Multiple missing data points indicate a process failure. The buyer should request a rework or reject the lot.
Do not rely on verbal assurances. The documentation is the only proof. If the foundry cannot provide the records, the process was not controlled. The risk of gas porosity is high. The risk of part failure is high. The risk of a production stoppage is high.
The goal of this audit is not to punish the foundry. The goal is to protect the part. A verified burnout and preheating process reduces the risk of defects. It also reduces the need for rework. It lowers the total cost of the part. It keeps the production line running.
Frequently asked questions
How do I know if the wax was fully removed before investment?
Check the wax recovery rate and burnout temperature logs. A consistent recovery rate and a temperature high enough to vaporize the wax indicate full removal. Look for residue on the mold after burnout.
What is the risk of skipping the preheating process?
Skipping preheating causes thermal shock. The mold can crack or the metal can solidify too fast. Both issues can lead to porosity or dimensional errors.
Can I verify burnout if the foundry uses a chemical process?
Yes. Check the chemical concentration and contact time. Verify the residue test results. If there is no residue test, the risk of incomplete removal is high.
What is a red flag for preheating?
A preheat temperature that is too high for the investment material is a red flag. It can cause delamination or cracking. A missing ramp rate record is also a red flag.
How often should I audit the burnout process?
Audit the process after any change in alloy, wax, or investment. Audit it when you see defects. Audit it when you switch foundries. A routine audit every quarter is a good baseline.


